Empowering Engineering Excellence: Innovate, Elevate, Deliver.
China’s MCB assembly automation sector includes manufacturers with different strengths in machine design, controls, integration, and after-sales support. A “top 10” list is most useful when it compares verifiable capabilities, not just promotional claims. Buyers should examine factory references, production-cycle data, changeover procedures, and the availability of spare parts. A polished demo is helpful. It is not proof of long-term performance.
For a transparent expert perspective, the following is an illustrative comment, not a quotation from a verified, named industry professional: “A reliable Mcb Assembly Robot should deliver repeatable assembly quality, with faults that operators can identify and resolve.” That practical test matters on the factory floor. Look closely at how each system handles component feeding, screw fastening, testing, and traceability. Ask whether the manufacturer can show those processes using the buyer’s actual MCB components. Small details count: a poorly positioned feeder or unclear alarm can interrupt a line. A little skepticism is healthy.
This article’s China top 10 overview can help readers build a shortlist, but rankings alone cannot establish suitability. Compare each supplier against your product range, target output, available floor space, and maintenance skills. Request specific evidence, then check it with customer references where possible. The best choice may not be the most elaborate cell. It may be the one your team can operate consistently, maintain safely, and adapt when product requirements change.
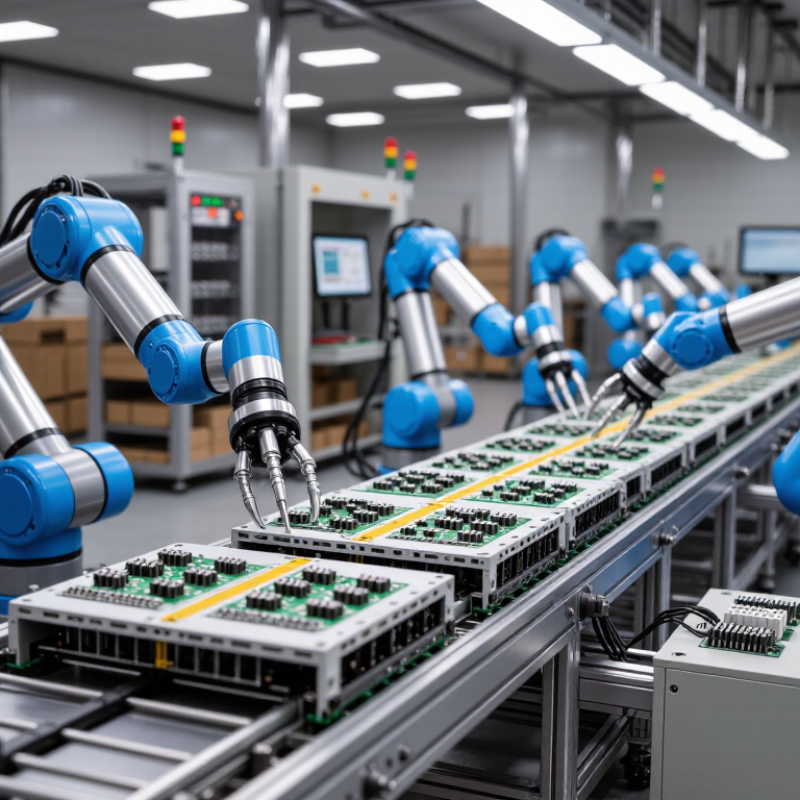
An MCB assembly robot is an automated system designed to build miniature circuit breakers with consistent speed and accuracy. It handles small parts such as housings, terminals, springs, contacts, and switching mechanisms. The robot does not replace every engineering decision. Instead, it performs repeated tasks under controlled conditions.
The process usually begins with a feeder that separates components and presents them in a fixed position. A vision camera checks orientation, missing parts, and visible defects. Robotic grippers then place each component into the breaker housing. Servo-driven tools control insertion force and fastening torque. This matters because a loose terminal can create heat, while excessive force may damage delicate parts.
After assembly, sensors verify movement, contact spacing, and switch operation. Electrical testers may check insulation resistance and trip performance under approved factory procedures. Data from each station can be linked to a production record, helping engineers investigate failures. In real production, dust, vibration, and inconsistent parts still cause trouble. No system is perfect.
A careful setup includes guarding, emergency stops, interlocks, and regular calibration. Operators also inspect tooling wear and review rejected units instead of trusting automation blindly. Small alignment errors can remain unnoticed for hours. That risk deserves more attention. A well-designed robot improves repeatability, but its results depend on accurate fixtures, stable materials, and disciplined maintenance.
Leading MCB assembly robot manufacturers focus on repeatability, traceability, and fast changeovers. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This growth reflects stronger demand for automated electrical assembly. However, robot quantity alone proves little.
A capable MCB system should position housings within tight tolerances. It should insert terminals, springs, toggles, and screws without damaging plastic parts. Servo-driven fastening needs torque monitoring, while machine vision checks missing or misaligned components. Critical details matter. The system should also record serial numbers, torque values, test results, and operator interventions. These records support process audits and practical troubleshooting.
Leading suppliers normally provide modular grippers, quick-change tooling, and recipe-based production control. A useful cell can switch between MCB ratings with limited downtime. Safety circuits should support guarded access, emergency stops, and risk assessments aligned with relevant machinery requirements. The IFR report also identifies electronics and electrical manufacturing as major users of industrial robots, reinforcing the value of compact, precise automation.
Yet some equipment specifications remain too optimistic. Published cycle times may exclude feeding jams, inspection rejects, or manual replenishment. Buyers should request acceptance tests using real components. They should measure first-pass yield, changeover time, noise, and maintenance access. A robot that looks impressive during a demonstration may still frustrate technicians on a crowded factory floor.
China’s Top 10 MCB Assembly Robot Manufacturers should be compared by production capability, not catalog size alone. Miniature circuit breaker assembly involves precise contact placement, spring loading, screw fastening, and electrical testing. Small alignment errors can affect consistency. Buyers should examine cycle time, changeover procedures, traceability, and after-sales engineering support using sample parts and factory trials.
The International Federation of Robotics’ World Robotics 2024 report recorded 276,288 industrial robot installations in China in 2023, about 51% of global installations. This indicates a substantial automation ecosystem, but the figure covers industrial robots broadly—not MCB assembly systems specifically. A manufacturer’s presence in China therefore does not prove specialist experience. Ask for process-level evidence: documented inspection results, uptime records, and examples of handling different breaker models. A neat ranking can be misleading. Actual line performance depends on product design, operator training, and maintenance discipline. Some comparisons remain imperfect because suppliers may define cycle time differently.
Technical reference chart for automated MCB assembly: IEC 60898-1 instantaneous tripping bands commonly used for B, C and D curve miniature circuit breakers. The chart contains no company or brand data.
B-curve MCBs trip magnetically at approximately 3–5 times rated current, C-curve devices at 5–10 times, and D-curve devices at 10–20 times. These technical ranges are relevant to inspection, testing and end-of-line automation in MCB production.
China Top 10 MCB Assembly Robot Manufacturers?
How to Compare MCB Assembly Robot Suppliers in China
Comparing MCB assembly robot suppliers in China takes more than reviewing a machine’s quoted speed. Ask how the system handles your actual miniature circuit breaker components, including small differences in housing size and terminal position. A useful supplier should explain its feeding, assembly, inspection, and rejection steps in practical terms. Request a sample run with your parts. Watch for missed screws, tilted components, and inconsistent test results. Numbers on a brochure are not enough.
Check the changeover time between product models, the availability of spare parts, and the training included after installation. Ask for cycle-time data from a comparable production setup, then confirm what was measured and what was excluded. It matters. A factory visit or live video demonstration can reveal cable routing, operator access, and how faults appear on the control screen. Also discuss acceptance criteria before ordering. Some details may remain unclear until your own components are tested; that is a real limitation, not a reason to skip testing. Compare written service response times, documentation, and support for future adjustments, not just the initial purchase price.
| No. | Comparison Dimension | What to Compare | Evidence to Request |
|---|---|---|---|
| 1 | Product and process coverage | Confirm which MCB assembly operations are included, such as component feeding, contact or arc-chute assembly, screw fastening, calibration, testing, marking, and packaging. The required process depends on the product design. | Process flow, station list, scope-of-supply document, and a demonstration using representative product components. |
| 2 | Product compatibility | Check supported pole configurations, frame sizes, component variants, and changeover requirements. Compatibility should be confirmed for the buyer’s actual drawings and tolerances. | Approved product matrix, tooling list, sample-run results, and written confirmation of exclusions or design limitations. |
| 3 | Automation and robot configuration | Compare the use of industrial robots, Cartesian systems, indexing tables, dedicated mechanisms, and manual loading. A robot is not necessarily required at every assembly station. | Machine layout, robot and controller specifications, station cycle sequence, and a description of safety interlocks. |
| 4 | Cycle time and line output | Evaluate cycle time against the required product mix and operating schedule. Output depends on product complexity, feeding stability, inspection steps, changeovers, and the number of parallel stations. | Time-study video, cycle-time calculation, stated assumptions, and a witnessed acceptance run using agreed product samples. |
| 5 | Quality and traceability | Check whether the system records process results and identifies rejected parts. Traceability may include product identifiers, test measurements, timestamps, and station or batch data. | Sample production records, data-field list, reject-handling demonstration, and details of data export or integration interfaces. |
| 6 | Electrical testing and standards | Confirm that test stations match the product specification and applicable destination-market requirements. IEC 60898-1 covers circuit-breakers for overcurrent protection for household and similar installations; IEC 60947-2 covers circuit-breakers for low-voltage switchgear and controlgear. | Test plan, instrument specifications and calibration records, applicable product-standard references, and customer-approved test limits. The machine itself does not establish product certification. |
| 7 | Tooling and changeover | Compare dedicated versus adjustable fixtures, the number of product changeover steps, tooling life, and the time needed to switch between variants. | Tooling drawings, changeover instructions, spare-tool quotation, and a demonstrated changeover using the intended product variants. |
| 8 | Controls and factory integration | Review PLC and HMI functionality, alarms, recipe management, safety controls, and available interfaces for connection to factory systems. Compatibility depends on the customer’s existing infrastructure. | Electrical schematics, I/O list, communications-interface details, alarm list, and a sample HMI screen or software demonstration. |
| 9 | Acceptance, installation, and training | Agree how machine performance will be verified before shipment and after installation. Acceptance criteria should specify products, run duration, quality checks, and responsibilities. | Factory and site acceptance test protocols, installation plan, training agenda, and a written list of acceptance criteria. |
| 10 | Service, spare parts, and total cost | Compare the full project scope rather than the equipment price alone. Include installation, shipping, commissioning, training, tooling, spare parts, software, and ongoing support terms. | Itemized quotation, recommended spare-parts list, warranty terms, service response arrangements, and documented support responsibilities. |
Comparison note: This table provides a supplier-evaluation framework, not a ranked list of manufacturers. Machine performance and supported products vary by project; verify all figures and capabilities against a written proposal and an agreed acceptance test.
MCB assembly robots support several critical production tasks, including component feeding, contact insertion, spring placement, screw fastening, and functional testing. A well-designed cell can position small parts within tight tolerances while maintaining steady cycle times. Vision systems check housing orientation, terminal presence, and visible defects. Torque-controlled tools reduce loose connections and damaged threads.
Selecting an MCB assembly robot requires more than comparing speed figures. Engineers should verify payload, repeatability, feeder stability, tooling access, and changeover time. The robot must handle different breaker ratings without creating excessive manual adjustments. Check whether the system records torque, insertion force, test results, and operator access events. Traceability matters during quality investigations. Safety guarding, emergency stops, electrical isolation, and risk assessment must match local regulations and site procedures.
Production trials reveal weaknesses that brochures often hide. Test real housings, springs, wires, and fasteners, not sample parts alone. Measure reject rates across several shifts. A cycle time may look excellent until feeder jams appear. I would also examine cleaning access and spare-part availability. These details affect uptime. No automation cell is perfect. Some low-volume lines may gain more from flexible tooling than maximum speed. A careful selection should balance quality, maintainability, worker safety, and future product changes.